In the food and beverage industries, maintaining high – level hygiene is of utmost importance to ensure product safety and quality. As a pneumatic diaphragm pump supplier, I am well – aware of the significant role our pumps play in these sectors and the strict hygiene requirements they must meet. Pneumatic Diaphragm Pump
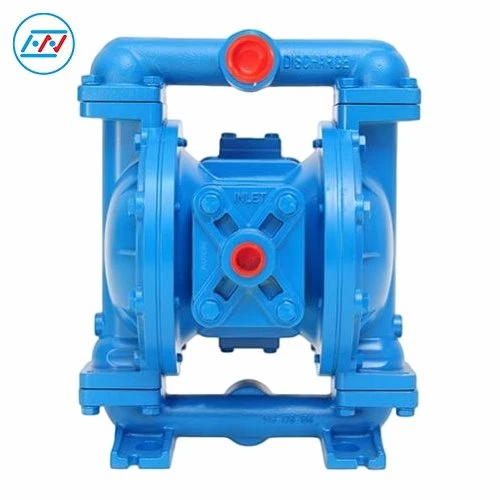
Material Compatibility with Food Products
The first and most fundamental hygiene requirement for a pneumatic diaphragm pump in the food and beverage industries is the material compatibility of all pump components that come into contact with the product. These components typically include diaphragms, valves, seals, and the pump body.
The diaphragms should be made from food – grade elastomers. Materials such as EPDM (Ethylene Propylene Diene Monomer), PTFE (Polytetrafluoroethylene), and NBR (Nitrile Butadiene Rubber) are commonly used. EPDM is popular for its excellent resistance to water, steam, and a wide range of chemicals, which is suitable for handling various food and beverage products. PTFE, on the other hand, is known for its non – stick properties, high chemical resistance, and ability to operate at high temperatures, making it ideal for applications involving viscous or sticky food products like syrups and honey. NBR offers good resistance to oils and fats, which is beneficial when dealing with dairy or oily food items.
Valves and seals also need to be crafted from food – compliant materials. Stainless steel, for example, is a widely used material for valve bodies and other metal parts. It is corrosion – resistant, easy to clean, and does not contaminate the food or beverage products. The seals should be made from elastomers that are approved for food contact, ensuring a tight and leak – free operation.
The pump body itself should be constructed from materials that can withstand frequent cleaning and sanitization processes. Stainless steel is again a top choice due to its durability, smooth surface, and resistance to corrosion. A smooth surface finish on the pump body is crucial as it prevents the accumulation of food particles, bacteria, and other contaminants.
Design for Cleanability
The design of the pneumatic diaphragm pump has a direct impact on its cleanability. A well – designed pump should minimize areas where food particles can get trapped, such as dead spaces, crevices, and sharp corners.
One important design feature is the use of a simple and open – flow path. The internal channels of the pump should be straight and unobstructed, allowing for easy passage of cleaning solutions and the removal of any residual product. This design also helps to prevent the formation of biofilms, which are communities of bacteria that can adhere to surfaces and cause contamination.
The pump should also be easy to disassemble and reassemble. This allows for thorough cleaning of all internal components. Quick – release clamps and fittings can be incorporated into the design to facilitate easy disassembly without the need for complex tools. For example, some of our pneumatic diaphragm pumps are designed with a modular construction, where individual parts can be easily removed and replaced for cleaning or maintenance purposes.
In addition, the pump should be designed to be compatible with various cleaning methods. It should be able to withstand high – pressure cleaning, chemical cleaning agents, and steam cleaning. The materials used in the pump should not be damaged by these cleaning processes. For instance, the food – grade elastomers should not degrade or swell when exposed to common cleaning chemicals.
Prevention of Cross – Contamination
Cross – contamination is a major concern in the food and beverage industries. A pneumatic diaphragm pump should be designed and operated in a way that prevents the mixing of different products or the transfer of contaminants from one batch to another.
One way to prevent cross – contamination is through the use of dedicated pumps for specific products. This is especially important when dealing with allergenic ingredients or products that require strict separation. Our company offers a range of pumps that can be customized to meet the specific needs of different food and beverage applications, allowing for the use of dedicated pumps for different products.
Another important measure is the implementation of proper cleaning and sanitization procedures between product changes. After each use, the pump should be thoroughly cleaned to remove any residual product. Sanitization processes should then be carried out to kill any remaining bacteria or microorganisms. This can involve the use of hot water, steam, or chemical sanitizers.
The pump should also be designed to prevent the backflow of product. Check valves can be installed at the inlet and outlet of the pump to ensure that the product flows in one direction only. This helps to prevent the mixing of different products and the contamination of the supply line.
Compliance with Industry Standards
Pneumatic diaphragm pumps used in the food and beverage industries must comply with a variety of industry standards. These standards are set by regulatory bodies to ensure the safety and quality of food and beverage products.
One of the most well – known standards is the 3 – A Sanitary Standards in the United States. These standards define the requirements for the design, construction, and operation of equipment used in the dairy, food, and beverage industries. Pumps that meet 3 – A standards are designed to be easy to clean, made from food – grade materials, and prevent cross – contamination.
In the European Union, the pumps must comply with the EU Food Contact Materials regulations. These regulations ensure that all materials that come into contact with food are safe and do not transfer harmful substances to the food. Our pumps are designed and manufactured to meet these and other international standards, providing our customers with the assurance that they are using equipment that meets the highest hygiene requirements.
Documentation and Traceability
In addition to meeting the physical and operational hygiene requirements, it is also important to have proper documentation and traceability. This includes providing information about the materials used in the pump, the manufacturing processes, and the results of any quality control tests.
We, as a pneumatic diaphragm pump supplier, provide our customers with detailed product documentation. This includes material certificates for all food – contact components, which verify the compliance of the materials with food safety standards. We also keep records of the manufacturing processes, including the heat treatment of metal parts and the molding of elastomers, to ensure traceability in case of any quality issues.
Furthermore, we conduct regular quality control tests on our pumps. These tests include performance tests, leak tests, and material compatibility tests. The results of these tests are documented and provided to our customers upon request. This documentation not only helps our customers to ensure compliance with industry regulations but also provides them with confidence in the quality and hygiene of our pumps.
Conclusion

As a pneumatic diaphragm pump supplier, I understand the critical importance of hygiene in the food and beverage industries. Our pumps are designed and manufactured to meet the strictest hygiene requirements, from the selection of food – grade materials to the implementation of proper design features for cleanability and prevention of cross – contamination. By complying with industry standards and providing detailed documentation, we ensure that our pumps are safe and reliable for use in these sensitive industries.
Pneumatic Diaphragm Pump If you are in the food and beverage industry and are looking for a high – quality pneumatic diaphragm pump that meets the highest hygiene standards, we would be delighted to have a conversation with you. Contact us to discuss your specific requirements and let us help you find the perfect pump solution for your business.
References
- 3 – A Sanitary Standards, Inc. Guidelines for Dairy, Food, and Beverage Equipment.
- European Union. EU Food Contact Materials Regulations.
Shaanxi Hono Electronic Technology Co., Ltd.
We are one of the most professional pneumatic diaphragm pump manufacturers and suppliers in China, featured by quality products and good price. With abundant experience, we warmly welcome you to buy customized pneumatic diaphragm pump made in China here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: 4C-1102, Financial Port, No. 1 West 1st Road, Fengjing Avenue, Fengdong New Town, Xi’an, Shaanxi, China
E-mail: juicy@honopump.com
WebSite: https://www.honopump.com/
